Pipeline Metal Detector
In industries where liquid, slurry, paste, and semi-solid products are processed, maintaining product purity is essential for quality assurance, regulatory compliance, and customer safety. Even the smallest metal contamination can lead to product rejection, equipment damage, production downtime, and reputational losses.
To eliminate these risks, manufacturers are increasingly adopting pipeline metal detectors that provide continuous in-line inspection of pumped products without interrupting the production process. Designed specifically for liquid and paste applications, these advanced metal detection systems help industries maintain high-quality standards while ensuring operational efficiency.
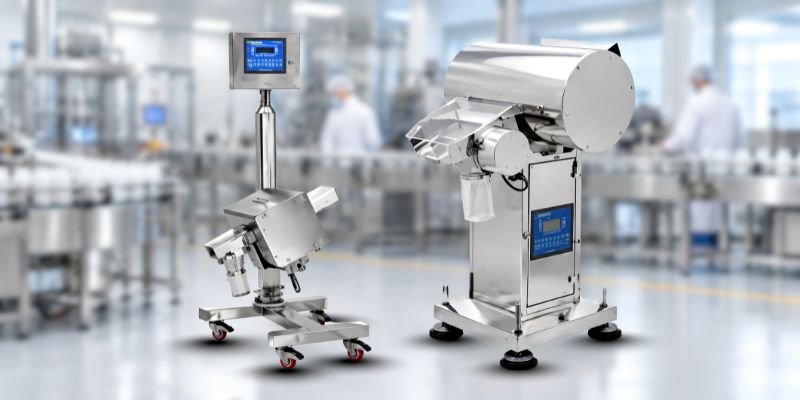
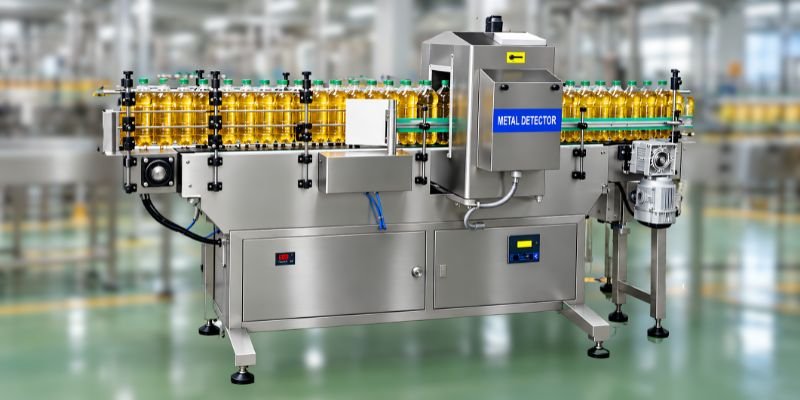
SMMS Engineering Systems offers high-performance Pipeline Metal Detectors engineered to detect metallic contaminants in liquids, pastes, slurries, pulps, and other flowing products with exceptional accuracy and reliability.
What is a Pipeline Metal Detector?
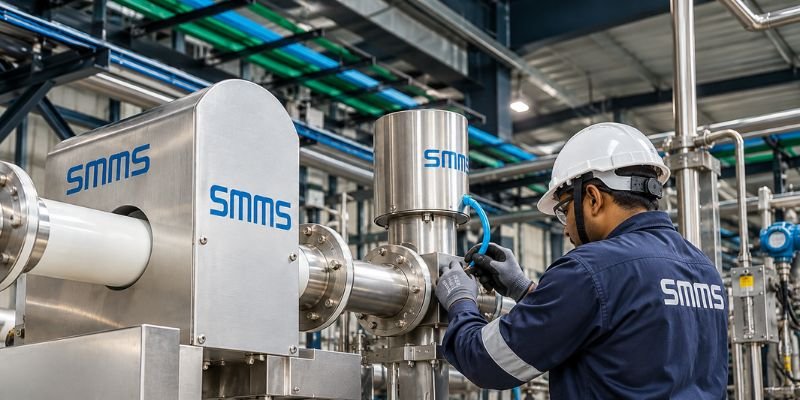
A Pipeline Metal Detector is an advanced inspection system installed directly into a production pipeline to detect and remove metallic contaminants from liquid, paste, slurry, and semi-liquid products during processing.
Unlike conventional conveyor-based systems, pipeline metal detectors inspect products while they are flowing through enclosed pipelines. The system continuously monitors the product stream and automatically rejects contaminated material without interrupting production.
These systems are widely used in pharmaceutical, chemical, cosmetic, dairy, beverage, and various industrial processing applications where contamination control is critical.
Why Metal Contamination Control is Critical in Liquid Processing Industries
Metal contamination can enter the production process through various sources, including:
- Equipment wear and tear
- Broken machine components
- Pumps and valves
- Mixing and processing machinery
- Maintenance activities
- Raw material contamination
- Pipeline corrosion
Even microscopic metal fragments can compromise product quality and damage downstream equipment. In highly regulated industries, contamination incidents can result in costly recalls, production losses, and compliance issues.
Implementing a reliable Pipeline Metal Detection System helps manufacturers identify and eliminate contaminants before products reach the packaging or distribution stage.
How Pipeline Metal Detectors Work
Pipeline Metal Detectors operate using advanced electromagnetic field technology.
As the liquid or paste product flows through a non-metallic inspection tube, the detector generates a stable electromagnetic field. When a metallic particle passes through the detection zone, it disturbs the electromagnetic field, creating a signal that is instantly detected by the system.
The detector then activates an automatic rejection mechanism, diverting only the contaminated product while allowing the remaining production flow to continue uninterrupted.
Modern Pipeline Metal Detectors can detect:
- Ferrous metals
- Non-ferrous metals
- Stainless steel contaminants
- Fine metallic fragments
- Machine wear particles
This real-time inspection process ensures effective contamination control throughout the production cycle.
Key Benefits of Pipeline Metal Detectors
1. Continuous In-Line Inspection
Pipeline systems inspect products during processing without stopping production, improving efficiency and reducing downtime.
2. Enhanced Product Quality
By removing metallic contaminants before packaging, manufacturers can maintain consistent product quality and customer satisfaction.
3. Protection of Processing Equipment
Metal fragments can damage pumps, filling machines, valves, and downstream equipment. Early detection prevents costly repairs and maintenance.
4. Reduced Product Waste
Modern rejection systems isolate only contaminated portions of the product stream, minimizing product loss.
5. Improved Compliance
Pipeline Metal Detectors help industries comply with stringent quality control and contamination prevention standards.
6. Increased Operational Efficiency
Automated inspection and rejection systems reduce manual intervention and improve production throughput.
Applications of Pipeline Metal Detectors
Pharmaceutical Industry
Pipeline Metal Detectors are widely used for inspecting:
- Liquid medicines
- Syrups
- Suspensions
- Gel formulations
- Pharmaceutical creams
- Ointments
These systems help pharmaceutical manufacturers maintain product purity and regulatory compliance.
Chemical Industry
Chemical manufacturers utilize Pipeline Metal Detectors for:
- Liquid chemicals
- Industrial solvents
- Adhesives
- Resins
- Specialty chemicals
The systems help prevent contamination while protecting sensitive processing equipment.
Cosmetics Industry
Metal detection is essential for:
- Creams
- Lotions
- Gels
- Shampoos
- Personal care products
Pipeline Metal Detectors ensure product safety and brand reliability.
Paints and Coatings Industry
Manufacturers use metal detectors to inspect:
- Paints
- Pigment slurries
- Coating compounds
- Industrial emulsions
Contamination-free products improve application performance and customer satisfaction.
Industrial Processing Applications
Pipeline Metal Detectors are also used in:
- Lubricants
- Polymer compounds
- Industrial pastes
- Chemical slurries
- Specialty formulations
Their versatility makes them suitable for a wide range of processing industries.
Food Industry
Metal detection is essential for:
- Pickles
- Fruit pulp
- Beverages
- Sauces
- Ready-to-use spice pastes
- Processed and packaged food products
Pipeline Metal Detectors ensure product safety, regulatory compliance, and brand reliability.
Features of Advanced Pipeline Metal Detection Systems
Modern Pipeline Metal Detectors are designed to meet demanding industrial requirements.
High Detection Sensitivity
Advanced technology enables the detection of extremely small ferrous, non-ferrous, and stainless-steel contaminants.
Hygienic Stainless-Steel Construction
SS304 and SS316 construction ensures durability, corrosion resistance, and suitability for demanding processing environments.
Automatic Rejection Mechanism
Integrated reject valves automatically remove contaminated products without disrupting production flow.
Digital Touchscreen Interface
User-friendly control systems simplify operation, monitoring, and reporting.
Custom Pipeline Sizes
Systems can be customized according to flow rates, pipe diameters, and specific production requirements.
Reliable High-Speed Performance
Pipeline Metal Detectors provide continuous inspection even in high-volume production environments.
Why Choose SMMS Pipeline Metal Detectors?
SMMS Engineering Systems has established itself as a trusted manufacturer of industrial metal detection solutions in India. The company’s Pipeline Metal Detectors are specifically designed for liquid and paste processing industries, offering exceptional sensitivity, reliability, and operational efficiency.
Key advantages of SMMS Pipeline Metal Detectors include:
- High detection accuracy
- Custom-built configurations
- Automatic reject systems
- Compact and robust design
- User-friendly operation
- Stable and reliable performance
- High-speed inspection capability
- Minimal product wastage
- Durable stainless-steel construction
SMMS works closely with clients to design and install customized metal detection systems that meet specific production and contamination control requirements.
Best Practices for Effective Contamination Control
To maximize the performance of Pipeline Metal Detectors, manufacturers should:
- Conduct regular system validation
- Perform routine maintenance and calibration
- Train operators on inspection procedures
- Monitor rejection reports and trends
- Schedule preventive maintenance
- Integrate metal detection into quality management programs
A proactive contamination control strategy significantly improves product quality and operational reliability.
Future of Pipeline Metal Detection Technology
As manufacturing processes become increasingly automated, Pipeline Metal Detection Systems are evolving with advanced digital technologies.
Modern systems now offer:
- Enhanced sensitivity
- Automated reporting
- Data logging capabilities
- Integration with production management systems
- Real-time monitoring
- Smart diagnostics
These advancements help manufacturers achieve higher levels of quality assurance while supporting Industry 4.0 initiatives.
Conclusion
Metal contamination remains one of the most significant challenges in liquid and paste processing industries. A single metal fragment can compromise product quality, damage equipment, and lead to costly production disruptions.
Pipeline Metal Detectors provide a reliable solution by delivering continuous in-line inspection, accurate contamination detection, and automatic rejection of affected products. By implementing advanced Pipeline Metal Detection Systems, manufacturers can improve product quality, protect equipment, reduce waste, and strengthen compliance with industry standards.
For industries seeking dependable contamination control solutions, SMMS Engineering Systems offers high-performance Pipeline Metal Detectors designed to meet the demanding requirements of modern manufacturing environments.
Contact SMMS Engineering Systems
Looking for a reliable Pipeline Metal Detector for your liquid, slurry, or paste processing application?
Contact SMMS Engineering Systems today to discuss your contamination control requirements and discover the right metal detection solution for your production line.